Showing posts with label weaving. Show all posts

Saturday, 17 October 2026

Bow and Skew in Woven Fabrics: Measurement, Causes and Cutting-Room Control


Imagine approving a checked cotton fabric by shade, weight and construction, only to find that its horizontal checks climb across a shirt front or curve around a kurta pocket. The fabric may be free of holes and stains, yet its geometry is unsuitable for the intended garment. Bow and skew deserve their own inspection decision because they concern the arrangement of yarns, not simply the dimensions of a rectangular piece.

Bow and skew are different distortions

Warp yarns normally run along the fabric length; weft yarns run across it. Bow describes curvature in the yarn path. Skew describes straight weft yarns lying obliquely rather than perpendicular to the warp. Both may occur together. A curved weft line can also change slope within the width, so checking only the two edges may miss local distortion. These distinctions underpin ISO 13015:2013.

Conceptual checked woven swatches showing curved weft lines and slanting straight weft lines

Conceptual comparison: bow curves the crosswise yarn path; skew tilts it. The illustrated distortions are exaggerated, not measured specimens.

Measure the yarn path, not an untidy cut edge

Lay the conditioned fabric flat without tension. Identify the actual weft path rather than assuming that a cut edge or printed stripe follows it. A pick glass helps distinguish yarn direction from surface decoration.

For simple overall skew, the principle is longitudinal displacement divided by the useful crosswise width, multiplied by 100. An illustrative 30 mm displacement across 1,500 mm gives 2%. This is a slope percentage, not an angle in degrees. Under ISO 13015, local skew requires assessment of the relevant portions rather than automatically using the full width as every denominator.

Bow concerns deviation from a straight reference joining the yarn’s ends. Record the method, reference length and units: a bow distance in millimetres is not automatically interchangeable with a buyer’s width-based bow percentage. Use the complete agreed standard for contractual testing.

Illustrative inspection of warp and weft yarns with a magnifier and textile pointer

Conceptual inspection scene: following an actual yarn avoids confusing structural distortion with the shape of a cut edge.

Three questions need different tests

A report should distinguish the fabric’s present geometry from changes caused by care and the behaviour of a sewn garment. The following methods address different questions; their percentages should not be substituted for one another.

Question Relevant method
How much bow or skew is present in the original fabric? ASTM D3882-08(2025), covering woven filling yarns and knitted courses
How does fabric skew change after home laundering? AATCC TM179-2025
How does a garment seam twist before and after home laundering? AATCC TM207-2025

This separation is particularly important when a mill supplies finished fabric but the garment maker subsequently launders the sewn product. The blog’s explanation of fabric and garment performance testing provides the broader approval context.

Look along the process, not only at the loom

Unequal tension across a fabric web can create distortion during manufacturing and wet processing. Therefore, finding bow in finished cloth does not prove that weaving alone caused it. Compare retained samples or measurements before and after key stages to locate where the geometry changes.

Mahlo’s technical overview identifies uneven tension distribution as a common source of unwanted distortion. For a practical investigation, check fabric entry alignment, the left-to-right tension balance, roller condition and the way the web enters and leaves finishing equipment. These are investigation points, not proof of a particular machine fault. Record the article, width, speed and process stage so that a later improvement can be traced to a controlled change.

Straightening requires feedback and verification

Industrial weft straighteners combine distortion detection with mechanical correction. Mahlo’s Orthopac documentation describes skew and bow rollers used for the respective corrections. Correcting one geometry should not be assumed to correct every irregular or changing distortion.

A sensible mill trial checks the incoming fabric, adjusts within the equipment supplier’s operating guidance, and verifies the output. Retain evidence of residual distortion rather than relying solely on a control-screen setpoint. Where washing is part of the product route, include the relevant after-care assessment. Temporary visual improvement is not enough if the customer’s approved appearance is lost later.

Denim is the important exception

Zero skew is not a universal objective. ASTM D3882 explicitly recognises applications where specified skew helps prevent trouser-leg twisting in twill fabrics. Intentional, controlled skew must therefore be distinguished from uncontrolled distortion. For denim, obtain the supplier’s approved target and assess the intended garment-washing route; do not apply an ordinary checked-shirting rule indiscriminately.

Turn inspection into a cutting decision

For Indian apparel sourcing, consider checked shirting, woven kurta fabrics and blouse materials separately. A small patch pocket, a long placket and a broad front panel expose different alignment problems. As a practical approval exercise, place representative pattern pieces on suspect fabric and make a sample rather than relying only on a small swatch.

Illustrative checked shirt front and separate pocket showing pattern-matching challenges

Conceptual cutting-room example: pocket and body checks need an agreed matching standard, not merely an acceptable average fabric result.

Agree tolerances by product and method before bulk purchase. ASTM D3882 notes that individual rolls are normally judged using their maximum distortion, rather than a favourable roll average. Keep roll identity and the positions of unacceptable sections. Rework, segregation or rejection should follow the agreed disposition; forcing distorted fabric into a lay is not a reliable correction. Link this decision to cutting-room control and recalculate usable consumption where pattern matching changes the marker plan.

Make supplier feedback reproducible. A useful defect record includes roll identity, useful width, position along the roll, direction of skew, maximum observed distortion, test method and care state. Photograph the yarn trace with a scale and retain labelled samples. If laboratories disagree, first compare specimen selection, preparation and calculation basis. The important question is whether both parties measured the same property on comparable material, not simply which report shows the smaller number.

Source acknowledgement

Sources checked on 17 October 2026: ISO 13015:2013 and its published preview; ASTM D3882-08(2025); AATCC’s method-selection guidance and 2026 Manual announcement, confirming TM179-2025 and TM207-2025; and Mahlo’s distortion-correction documentation. The calculation and sourcing examples are explanatory, not acceptance limits. The three original AI-generated illustrations are conceptual and do not represent laboratory results.

Tuesday, 5 May 2026

Why You Can’t Make the Same Fabric “Just a Little Finer”


Altering Fabric Weight, Fineness, and Coarseness

In woven cloth, the final character of the fabric depends on several connected factors. These include the yarn count, the number of ends per inch, the number of picks per inch, and the weave or pattern used in the cloth.

The important point is this: you cannot change only one property of a fabric without affecting the others. If the weight, fineness, yarn count, thread density, or weave structure is changed, the character of the fabric will also change in some way.

Technical Note:
A woven fabric is not merely a collection of yarns. It is a balanced structure in which warp, weft, yarn thickness, thread spacing, and weave interlacement work together.

1. Main Factors That Decide Fabric Character

The character of a fabric is mainly controlled by four constructional factors:

Factor Meaning Effect on Fabric
Yarn count Fineness or coarseness of warp and weft yarns Affects weight, handle, cover, strength, and appearance
Ends per inch (EPI) Number of warp threads per inch Controls warp density, cover, compactness, and firmness
Picks per inch (PPI) Number of weft threads per inch Controls weft density, surface feel, warmth, and compactness
Weave or pattern Plain weave, twill, satin, basket weave, rib, etc. Controls interlacement, surface effect, flexibility, drape, and texture

These four factors are interdependent. If one is changed, the others usually require adjustment. A cloth cannot be made heavier, lighter, finer, or coarser in isolation while keeping everything else exactly the same.

2. Altering Cloth Weight While Keeping the Same Character

When we say that a cloth is to be made heavier or lighter while retaining the same character, we mean that the basic structure and appearance should remain similar.

For example, suppose we have a cotton drill fabric and the buyer says:

“Make the same drill fabric, but heavier.”

The designer cannot simply add more weight without disturbing the structure. To increase weight while maintaining the same type of fabric, both the yarn count and thread density must be adjusted.

A heavier fabric generally requires coarser yarns, suitable adjustment in EPI and PPI, maintenance of the same relative balance between warp and weft, and preservation of the original weave character.

Similarly, if the fabric is made lighter, it will usually become finer. This means finer yarns and lower total material per square yard or square metre.

Practical Note:
If more weight is obtained while preserving the same structure, the cloth generally becomes coarser. If less weight is obtained, the cloth generally becomes finer. But the basic character of the fabric should still remain recognizable.

For example, a heavier twill should still look and behave like a twill. A lighter poplin should still retain the basic poplin character.

3. Why “The Same Fabric, but a Little Finer” Is Not Fully Possible

There is a very practical example. A buyer may say:

“I want exactly the same thing, but a little finer.”

Technically, this is not fully possible. If the cloth is made finer, at least one fabric variable must change. The fabric weight may change, the yarn count may change, the EPI or PPI may change, the warp-weft balance may change, or the weave structure may change.

Therefore, the fabric cannot remain exactly the same and also become finer. At best, the designer can create a fabric that gives the appearance of greater fineness while keeping the weight nearly the same. But even then, some structural adjustment is involved.

4. Fineness Can Be Increased Without Much Change in Weight

Sometimes a fabric can be made to appear finer without reducing its weight in any major way. This is usually done by changing the relation between warp and weft.

For example, the designer may use a finer weft yarn with more picks per inch, or a finer warp yarn with more ends per inch. Another method is to make the cloth closer in one direction so that it appears smoother, denser, and more refined.

This may even improve the fabric. If increased fineness is obtained while maintaining weight, the fabric may become closer, more compact, warmer, and better covered. This is especially useful in clothing fabrics where warmth and compactness are desirable.

5. Difference Between Weight, Fineness, Coarseness, Compactness, and Cover

It is useful to distinguish between these related but different fabric properties.

Property Meaning How It Is Usually Changed
Weight Mass of fabric per unit area By changing yarn thickness, EPI, PPI, or weave
Fineness Delicacy or refinement of fabric surface By using finer yarns, closer setting, or smoother structure
Coarseness Heavier, thicker, rougher, or more open character By using coarser yarns or different thread spacing
Compactness Closeness of yarn arrangement By increasing EPI or PPI
Cover How well yarns hide gaps in the fabric By increasing yarn diameter or thread density

A fabric may be heavy but fine-looking, or light but coarse-looking, depending on how the yarns and structure are arranged.

For example, a fine wool suiting may be heavy but smooth in appearance. A loosely woven coarse cotton fabric may be light but still look rough. Chiffon is light and fine. Canvas is heavy and coarse. Satin may appear fine because of its smooth surface, even if it has considerable weight.

6. Altering Both Weight and Fineness Together

The most difficult problem is to increase both weight and fineness at the same time.

Normally, increasing weight tends to make a fabric coarser, while increasing fineness tends to reduce weight. Therefore, to obtain both increased weight and increased fineness, the designer must alter the relation between warp and weft very carefully.

7. Method: Make One Set of Threads Coarser and the Other Finer

One possible method is to make one yarn system, either warp or weft, much thicker and reduce its quantity proportionately. This creates more space between those threads. Then the other yarn system can be made finer and inserted in much greater quantity.

For example, the warp may be made thicker and more open. Because there is more space between the warp threads, a greater number of fine weft picks can be inserted. The coarse warp contributes to fabric weight, while the closely packed fine weft gives a smoother and finer-looking surface.

In such a construction, the fine weft may cover the coarse warp so completely that the coarse warp is almost hidden from sight.

Design Insight:
A fabric can become heavier because of hidden or partly hidden yarn bulk, while still appearing fine because the visible surface is dominated by finer, closely packed yarns.

8. Reverse Method: Fine Warp and Coarser Weft

The same principle can also be reversed. Instead of using a coarse warp and fine weft, the designer may use a finer warp and a heavier weft, depending on the required surface effect.

This depends on whether the fabric is intended to be warp-faced, weft-faced, compact, soft, firm, decorative, smooth, or textured.

Fabric Effect Required Possible Construction Approach
Fine surface with weight Use fine visible yarns with hidden heavier yarn contribution
Dense warm fabric Increase picks or ends in one direction
Smooth warp-faced fabric Use more warp cover and suitable weave
Weft-faced compact fabric Use more weft cover and higher PPI
Rich decorative surface Use supplementary warp or supplementary weft
Heavier saree feel Use denser yarn insertion, zari, or heavier ground construction

9. Importance of Weave Structure

The method described above has limits. If the difference between warp and weft becomes too great, the fabric may become unsatisfactory.

For example, if the warp is too thick and the weft is too fine, or if the weft is too thick and the warp is too fine, problems may arise. The fabric may show poor interlacement, uneven surface, weak construction, poor handle, excessive cover in one direction, weaving difficulty, distorted pattern, or poor dimensional stability.

The weave structure must support the relationship between the yarns. A plain weave has many interlacements and may not easily allow heavy packing of threads. A twill or satin has fewer interlacements and may allow more yarn packing, but it will also change the appearance and performance of the cloth.

Common Confusion:
Changing yarn count or thread density is not merely a numerical adjustment. It changes the actual behaviour of the fabric: its feel, fall, cover, warmth, strength, and appearance.

10. Practical Example: Cotton Shirting

Suppose a buyer has a cotton shirting fabric and says:

“I want the same fabric, but heavier and finer.”

This request is contradictory unless the construction is changed intelligently. The designer may use finer visible yarn in one direction, higher EPI or PPI, closer cover, or a slightly adjusted weave. The fabric may now look smoother, finer, and more compact while also becoming heavier.

However, it will not be exactly the same fabric. It will be a modified fabric with a similar character.

Existing Fabric Possible Modified Fabric
Medium yarn count Finer visible yarn in one direction
Moderate EPI and PPI Higher EPI or PPI
Ordinary cover Closer cover
Moderate weight Increased weight through hidden yarn bulk or compact setting
Same weave Slightly adjusted weave or density

11. Practical Example: Saree Fabrics

In saree design, this principle is extremely relevant. A buyer may say:

“Make the saree lighter but keep the same fall and richness.”

This is not easy, because richness often comes from yarn density, zari content, fabric cover, border weight, pallu construction, and finishing treatment. If weight is reduced, the saree may lose body, fall, or richness.

Similarly, a buyer may say:

“Make it more premium-looking but do not increase weight.”

This may require finer yarn, better finishing, increased lustre, smoother weave, better colour depth, improved zari quality, or a more compact but lightweight construction.

So the textile designer must decide which fabric property is being altered and which property must be preserved.

12. Central Principle

The central principle can be stated simply:

A woven fabric is a balanced structure. Weight, fineness, coarseness, compactness, yarn count, thread density, and weave are all connected. Changing one property inevitably affects the others.

Therefore, in fabric development, the correct question is not merely:

“Can we make this fabric heavier?”
“Can we make this fabric finer?”

The better question is:

“Which fabric character must be preserved, and which construction variables can be changed?”

13. Simple Summary

When This Is Changed What Usually Happens
Weight is increased Fabric generally becomes coarser unless construction is carefully modified
Weight is reduced Fabric generally becomes finer or lighter in character
Fineness is increased Weight, density, or warp-weft relation must change
Both weight and fineness are increased One yarn system may be made heavier while the other becomes finer and more closely packed
Weave structure is changed The original fabric character may also change

Conclusion


Altering the weight, fineness, or coarseness of a cloth is never a single-variable exercise. A woven fabric is a structural balance between yarn count, ends per inch, picks per inch, warp-weft relation, and weave pattern.

A fabric can be made heavier, lighter, finer, or coarser, but each change has consequences. The skill of the textile designer lies in making these adjustments while preserving the desired character of the cloth as far as possible.

In practical fabric development, especially in apparel, shirting, suiting, sarees, and furnishing fabrics, the most important question is not whether a fabric can be changed, but how much change can be made without losing its identity.

Buy my books at Amazon.com

Wednesday, 11 June 2014

Nuapatna Ikat Textile Cluster-3


This one is called the Khandua Society.

Khandua fabrics and Sarees are in general products woven in the Nuapatna Cluster.

Was impressed to see the technical innovation done in handloom to ease the life of weavers. Use of pedal, chain and wheel from cycle to adoptation of Tara loom to weave weft ikat is amazing. Have a look.


In general in all these sarees the border portion is weft tyed-died while the body portion in weft ikat. 

To know more read the document in this journal

Tuesday, 10 June 2014

Nuapatna Ikat Textile Cluster-2


This cluster specializes in making Dongria and Siminoi Sarees, which are woven motifs inspired from the embroidery and colors used by Dongria and Siminoi tribes of Orissa.

Dongria


Siminoi


Apart from the that traditional Ikat sarees were woven. EPI x PPI for Silk sarees is 88x 80 for Cotton it is 70 x 80.

The count used in Silk is Bangalore x Maldah ( 20/22 degummed x 33/37 degummed) for Cotton it is 120s x 2/100s.

Monday, 9 June 2014

Nuapatna Ikat Textile Cluster


Nuapatna

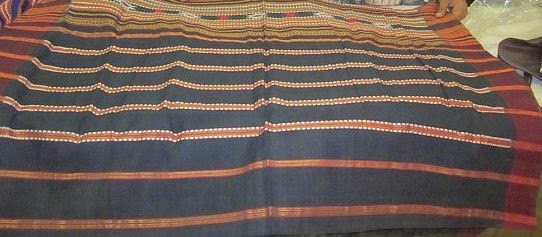
This place is known for its Ikat Textiles, specially Sarees. The ikat used is weft Ikat.

When we reached, it was a hot summer day with temperature soaring up to 45 deg C with humidity. But looking at the "cool" weaving, took away some of the heat.

Frame looms are used to weave.

Look at the "bow" used to control the weft, this gives wavy selvedge to the saree. Considered by some as a defect,this is inherent to the manufacture of this saree.


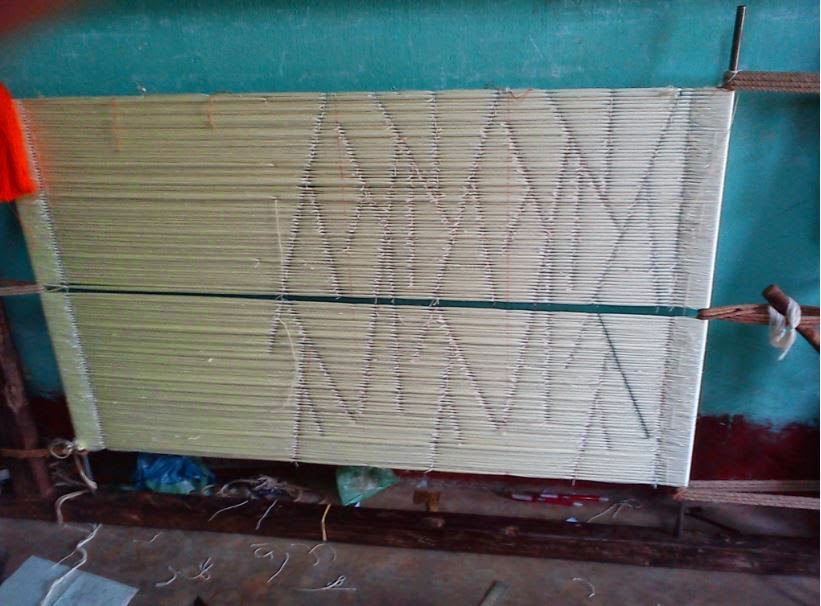
Frame used to tie and dye the weft yarn. The pattern is prepared on the frame then it is transferred to weft spools and then these are used in the loom for weaving. 


The count used is 2/100s or 2/120s for cotton. Both mercerised and non mercerised cotton is used. Silk used is Bangalore (20/22 denier degummed) or Maldah Silk (30/33) denier Mulberry. In Nuapatna Generally Bangalore Silk is used in the warp and Maldah is used in the weft. 


Note the "Comb" used at the selvedge to control the border ends. Note also the absence of warp stop motion. Which means weavers eyes are the only instruments to detect a defect, and it one can only spot a missing end ( Chira) in a 2/100s count cotton only after a few picks have been woven. So expect some missing ends in the warp.


Throughout India, home made dobby attachements are used to create the design. Here is the Nuapatna version.


Notice the lingos falling down at the border.


To create this design below the following steps are done:

1. White fabric is ties for the first time
2. Then it is dyed in the motif colorr. ( Fawn)
3. Then the motif only is tied.
4. Then it is treated with hydro ( Sod. Hydrosulphide) to take away the color from the remaining portion- if needed.
5 Then the background is dyed. 


Generally acid dyes are used for silk and vat dyes for cotton. However, the characteristic "red" of Ikat will bleed as it is dyed in napthol color. For all the bright colors napthol dyes are used, which may bleed. They have also started using the reactive dyes, but is it very rare. 

Do you see the little zig-zag line at the left side in the picture above , this is how the weavers control design, they make sure that this zig-zag line is maintained by pinching a small amount of weft. which is shown as a loop in the wrong side of fabric. So mind you, if you get those loops of yarn at the side of the fabric, these are not defects but effects inherent to the weaving technique. 

This is Nuapatna No. 1, there are many more such societies. Surprisingly each have a different language of products. 


This society has an elaborate stand for checking the sarees against the light. 


Saturday, 5 April 2014

Powerloom Clusters in India- A case of Tamil Nadu


The following are some of the observations:

1. The average production of grey fabric per loom per day is 30 meters.

2. For grey varieties, the beam length is observed to be of 1000 meters and max of 4750 meters.

3. For Sarees, the beam length is of 400 meters to 1000 meters.

4. 50% of the powerlooms operate in one shift and 50% in two shifts. As the powerlooms are working on jobwork basis, and they switch over to two shifts only if the jobwork is available. Also there is a restriction on the working of powerloom in the nights. The number of working hours for the units with one shift is 10 to 12 per day. Those which are working in two shifts work from 8 to 10 hours per day.

5. In case of sarees the powerlooms work in one shift only due to the design restrictions.

6. 95% of the units work in the range of 20-25 days in a month. In a year, 90% of the units work for 10 months and above.

7. In grey fabric production one weaver attend to normally 6 looms, if there are no dobby or jaquard deign. For all yarn dyed fabric, one weaver attends to about 2 looms. For sarees, it is one loom pere weaver.

There are two types of Production Activities followed:

1. Job work Units producing Greige Fabric

2. Entrepreneurial Units carrying out own production

In 1. The warp beam and the weft yarn is provided by the master weaver. The fabric is converted and supplied back to the master weaver.

In this case there are several disadvantages: As the job work unit supply the grey fabric without inspection, the quality of the fabric may not be best and depends upon the available infrastructure and resources.

As there are no inspection facilities so feedback is not scientific. Absence of stop motions - warp and weft as well as untrained weavers create a lot of defects. The product may have stains due to incorrect handling by weavers. Improper ventilation and housekeeping leads to lot of foreign matter in the end product.

In 2. The yarn is procured, dyed and converted.

The flow chart of the various production models are as given below:


source

Saturday, 2 February 2013

Buying of Indian Ethnic Fabrics- Weaving Issues


Weaving flaws come naturally with Indian traditional fabrics. Some of these are inevitable and some of these are avoidable. Below are the details of the common weaving issues that come with the Indian traditional fabrics:

Fabric Weight
Weaving defects in the traditional fabrics arise due to techniques used in weaving them as well as the manual operations involved in it. They also occur as the quality of yarn used in warp and weft is compromised or the yarn itself is handspun. In Handloom fabrics, the usual defects are holes, mending, missing end and missing and broken picks. The fabric weight also varies as the fabric is getting woven with variable beat up depending upon the person and also varies during the course of the day of weaving. In the morning, the weaver is fresh, and the beat up is more compact. As the day progresses the picks may spread farther apart.
From the facts given above, it can be inferred. The usual method of finding GSM by using GSM cutter is no longer valid when evaluating handloom fabric. The best way to evaluate is to weight it thaan by thaan and average it out. 


Chira ( Missing End)
This effect occurs in all the fabrics, but it is more severe in powerlooms which are without warp stop motion. Chira is not prevalent in South looms as they are equipped with warp stop motion. However, for woven fabrics of north India, it is quite a common defect. 


Banding
Banding in the weft occurs due to particular contrast of colors, it is more visible in fabrics with cross colors. Also banding is visible when yarns are hand dyed and after the finish of one pirn, the next pirn contains different dyed lot of yarn. It also is visible in dyed fabrics when the count in the weft changes appreciably. It is more common in Khadis where the yarns of weft ( Amber) come in different lots. 


Tight End and Reed Mark
This forms a series of warp wise faint lines in the fabric. It occurs due to uneven tension in the warp beam which can happen when making the warp beam manually. It also occurs due to not cleaning, damaged heald wires or some problems in the reed. Often reed marks come in these fabrics. 


Holes
The main cause of holes is the pointed scale used all across the country to measure the length and fold the cloth. If a center point is used to hold the fabrics, and the point gets blunt it can cause appreciably visible holes and sometimes makes the whole fabric amenable to rejecting. 


Slippage of the Warp or weft ends
This takes place in almose all the fabrics loosly woven but it is more appreciable in silks and especially unions of silks with Viscose. The unions from Bhagalpur are more susceptible to this defect. To counter this the fabric after weaving is given a special starch finish, but that too is unsustainable and gives way in three or four washes. The cause of this defect is the smooth surface of viscose which can slip easily on silk. This damage leads to seam slippage which is easily noticeable in the stress areas of the garment(neck and arm whole) The solution is to improve the construction of the fabric or use a better quality viscose. To control this problem in garments at the nect, moon patches are applied


Specs
This defect is observed in handloom fabrics which use handspun yarn. Based on the quality of roving they are using these will contain foreign fibers which do not catch dyes leading to this defect. 


Rough appearance
Rough appearance occurs due to the nature of yarn. In most of the cases carded yarn is used, which contain short fibers which come at the top in the process of weaving. This also due to the uneven count of yarn and slubs present therein. This defect is not a defect as such rather than a mark of true ethnic fabrics. Moreover, hand feel of two garments made from identical fabrics will be different as they may be woven on different looms and subject to different treatments.


Pilling
Pilling in cotton fabric is observed in cross colors where one of the yarn is of dark color. The short fibers come to the surface and form a pill type structure. This defect is aggravated when one of the yarns is sulphur dyed. This is also present in Matka silk which is handspun and handwoven. In yarn dyed Matka, the problem is further aggravated. Silk Noil fabrics are also a victim to this defect as they by default contain short fibers.  

Sunday, 3 June 2012

Manufacturing of Powerloom 40s x 40s 72 x 68 Fabric


This fabric is woven on the border areas of Andhra Pradesh and Tamil Nadu states of India and has a widepopularity as a dress material for ladies ( Kurtis and Salwars). It has the potential to be printed or embroidered.

The count for this fabric is 40s  both warp and weft and constructions is 72 and 68. It is available in both 44 inches and 56 inches.

The following are the broad steps in making the fabric

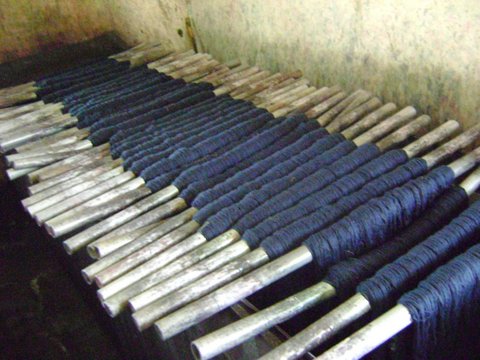
1. Yarn is taken in hank form and is kept in water tanks for two days for them to wet properly. Then the yarn is scoured in hank form itself.

Label on a Hank Yarn


2. Yarn dyeing is done using either reactive or vat dyes. Yarn dyeing is done manually.
Color Kitchen

Dyeing Bath for Hank Yarn - Reactive Dyes
  

3. Yarn is then subjected to sizing using Maida and Gum as components. The yarn is subjected to alternate dyeing and sizing three times.
Yarn Being Dried after Sizing

4. Yarn is then prepared for warping using an ingenious creel and then wound onto a weavers beam using a conventional sectional warping machines. 


5. Pirns are prepared using an indigenous contraption.


6. Yarn is then worked on powerloom having warp stop and weft stop motion.


6. Primitive dobbies are used for woven and zari borders.
 
7. The yarn is then subjected to finishing using water, sometimes in a padding mangle using softner and desizing agent.


Thanks for your attention. Did you find the information you were looking for ? Please leave a comment. Do you need to know more ? Please suggest a topic in the comments. You can also join the Forum for your specific queries.

Total Pageviews